

A packaged ultrafiltration and reverse-osmosis plant will only run at a remote mine camp if the raw water, the pre-treatment, the recovery, the disinfection and the people who will operate it are all up to the specification – not just the daily volume and a container size, Victor Zhang* writes.
A small plant, a long way from town
A remote mine camp often takes its drinking water from a borehole, a well field or a nearby surface source, and treats it in a container or on a skid. The enquiry typically starts with two figures: how many cubic metres a day the camp will need, and how salty the water looks on a laboratory sheet. Both matter. Neither decides whether the plant will still be running six months after handover.
This is a general technical discussion for engineers and camp-services managers, not a project case study, and it does not report site results. The gaps discussed below are specification and design gaps that are familiar on packaged membrane plants; they are not a claim about any named mine.
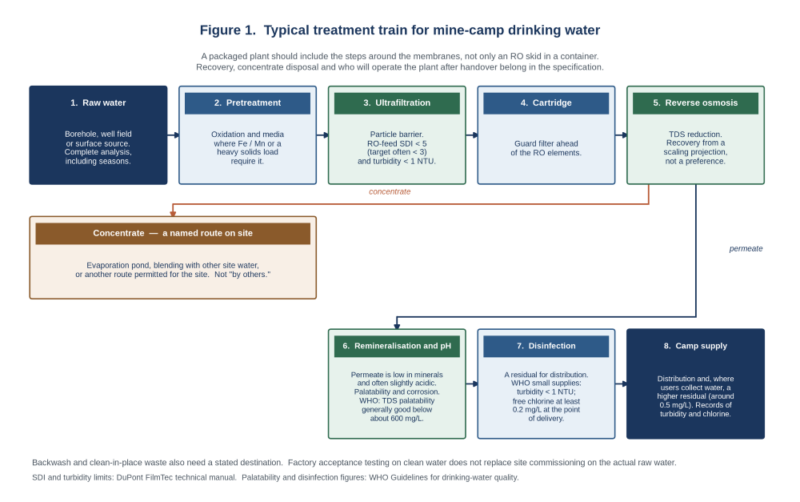
The usual train is straightforward: pre-treatment, then ultrafiltration (UF) where a tight particle barrier is needed, then reverse osmosis (RO) where dissolved solids have to come down, then re-mineralisation and disinfection before the water enters the camp distribution (Figure 1). A container that holds only an RO skid, with the rest left for “site installation,” is often where the trouble starts.
The raw-water sheet is usually too thin
Membrane plants fail first on the water they were not told about. A total dissolved solids (TDS) figure and a pH are not a design basis. The enquiry should include turbidity, the silt density index (SDI) where it can be measured, iron and manganese as both total and dissolved, hardness, alkalinity, sulphate, barium, strontium, reactive silica, organics, temperature and whether the sample is from the dry season, the wet season, or a well that has only just been pumped.
Anoxic groundwater often carries dissolved iron and manganese that are invisible in a fresh sample. Once they meet air or an oxidant, they form particles that plug cartridges and the lead RO elements. UF retains those particles; it does not remove dissolved Fe²⁺ or Mn²⁺. Hardness and reactive silica are also unaffected by a particle filter. They concentrate in the RO reject in proportion to the concentration factor, 1/(1 − recovery). At 75% recovery that factor is 4; at 80% it is 5; at 85% it is about 6.7. A water that looks comfortable at 70% recovery can be against a silica or carbonate limit at 80%. Recovery is the output of a scaling projection, not a preference written into a tender because well yield is tight or a pond is small.
Seasonal change is the other common omission. The same well field, or a blend with surface water after rain, often shows a rise in turbidity and a shift in iron. A train designed only around a dry-season sample is often the one that struggles first after handover. Samples should be taken after the borehole has been pumped long enough to be representative, and each well that may be used needs its own data.
Pre-treatment and the limits the RO actually sees
Spiral-wound RO elements are not a substitute for pre-treatment. Membrane manufacturers commonly require the 15-minute SDI of the RO feed to be below 5 and recommend a lower working target, often below 3, together with a feed turbidity below 1 NTU. What matters is whether the filtrate stays inside those limits after backwash and after a change in season, not a single good result on a clear day.
Multimedia filtration is often sufficient when the raw water is consistently low in turbidity and the filtrate meets those limits with a clear margin. It is not a tight physical barrier: after backwash the bed is still settling, and a pulse of solids can reach the cartridges. UF, usually in hollow-fibre form, is the more reliable barrier when the water is variable, attendance is limited, or a consistently low-SDI feed is required. Published work on integrated membrane systems typically reports UF filtrate turbidity of the order of 0.04 to 0.1 NTU and SDI values commonly of about 0.3 to 2 in normal operation. Those figures are typical practice, to be confirmed on the actual water, not a performance guarantee.
The specification should say which barrier is required, how it will be cleaned and how backwash, cleaning waste and concentrate will be handled. Even a modest camp plant producing, for illustration, 100 cu.m/d of permeate at 75% recovery will discharge about 33 cu.m/d of concentrate. At a remote mine that volume has to go somewhere − an evaporation pond, blending with other site water, or another route permitted for the site. Leaving it as “by others” is how a plant that works on paper cannot be started.
After the membranes: water the camp can actually drink
RO permeate is low in dissolved minerals and is often slightly acidic. It can be unpalatable and aggressive to pipes and heaters. The World Health Organization (WHO) has not set a health-based guideline value for TDS; it notes that palatability is generally considered good below about 600 mg/L and that water becomes significantly and increasingly unpalatable above about 1,000 mg/L. Re-mineralisation − typically a calcite contactor or a controlled dose of calcium and alkalinity − and pH adjustment belong in the train, not as a later extra.
Disinfection after the membranes is equally part of the plant. UF and RO reduce microorganisms, but they do not leave a residual for the distribution system. WHO guidance for small supplies is to keep turbidity below 1 NTU for effective disinfection (and below 5 NTU if that target cannot be met), to maintain a free chlorine residual of at least 0.2 mg/L at the point of delivery, and to raise that residual to around 0.5 mg/L where users collect and store the water themselves. For chlorination to work as intended, pH should be below 8, with a usual working range of about 6.5 to 8.5. A camp that skips this step, or that cannot measure residual chlorine and turbidity after start-up, is relying on the membranes alone for a duty they were not designed to carry.
The container, the power and the people
A container is a convenient way to ship a plant. It is also a small room that can overheat, freeze, collect dust and lose power. FilmTec elements, for example, have a normal feed-temperature limit of 45°C. In a closed box in a hot climate, the air around the panels, pumps and membranes can exceed what the equipment was designed for. The specification should cover insulation, ventilation or air-conditioning, freeze protection where needed and access to change a cartridge or a membrane without dismantling the container. Power quality belongs there too: high-pressure RO pumps and variable-speed drives do not take kindly to a generator that sags or spikes.
Redundancy is a camp-services question, not a luxury. If the camp cannot be without water, duty and standby pumps, and enough capacity to run while one train is cleaned, should be stated in the enquiry. So should a commissioning spare-parts list: cartridges, anti-scalant, cleaning chemicals, seals and at least one spare membrane element. A plant that waits six weeks for a filter cartridge is not a reliable camp supply.
Factory acceptance testing (FAT) is necessary and is not sufficient. FAT is usually run on clean water: it proves that the skid starts, the instruments read and the control sequence works, but not that the pre-treatment can handle the borehole. Site commissioning on the actual raw water, with the operating staff present and a manual that states cleaning triggers in measurable terms – pressure drop, normalised flow, SDI, residual oxidant – is what closes the job. If attendance after handover will be limited, that is a design input: it argues for a more robust barrier, clearer interlocks and, where communications allow, remote monitoring of flow, pressure and conductivity.
What the specification should cover
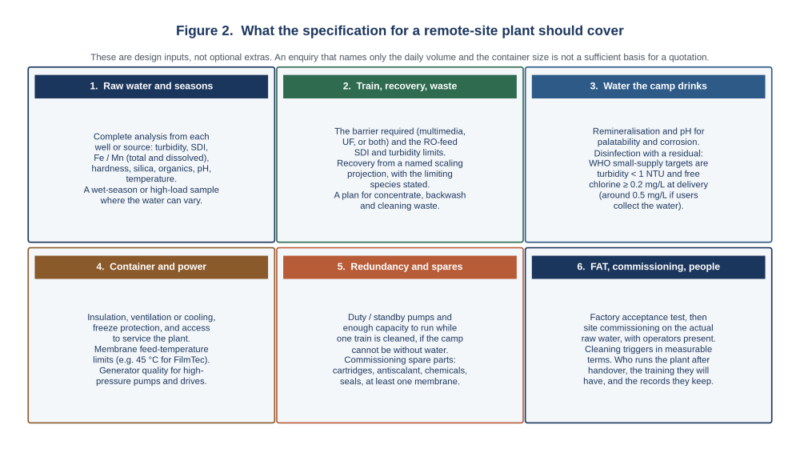
The items above can be written into a short specification (Figure 2): a complete raw-water analysis from each source, including a wet-season or high-load sample; peak and average demand; the treatment train and the RO-feed limits it must meet, with recovery tied to a named scaling projection and a stated plan for concentrate; post-treatment for palatability, corrosivity and disinfection; the container environment and power supply; and redundancy, spare parts, FAT, site commissioning on the raw water, and who will operate the plant after handover. None of this requires an unusual plant. It requires the enquiry to describe the water, the site and the people, rather than only the daily volume and the size of the box.
Conclusion
A containerised UF/RO plant is a sound way to supply drinking water at a remote mine camp, provided the specification is as complete as the site is remote. Plants in this duty more often fail because the raw water was incompletely described, the pre-treatment or the recovery was optimistic, disinfection and re-mineralisation were left out, or no one on site was prepared to run the plant, than because the membranes were the wrong product. The enquiry that names those things is the one that is worth answering.
*Victor Zhang is Sales Manager at Guangzhou Globaluf Water Treatment Co., Ltd. (GlobalUF), Guangzhou, China, and has worked in the water treatment industry since 2009. The company, founded in 2005, designs and manufactures ultrafiltration, brackish-water and seawater reverse osmosis, and containerised water-treatment systems
The post Exploring mine camp drinking water from containerised ultrafiltration and reverse-osmosis plants appeared first on International Mining.